Never stop the filler
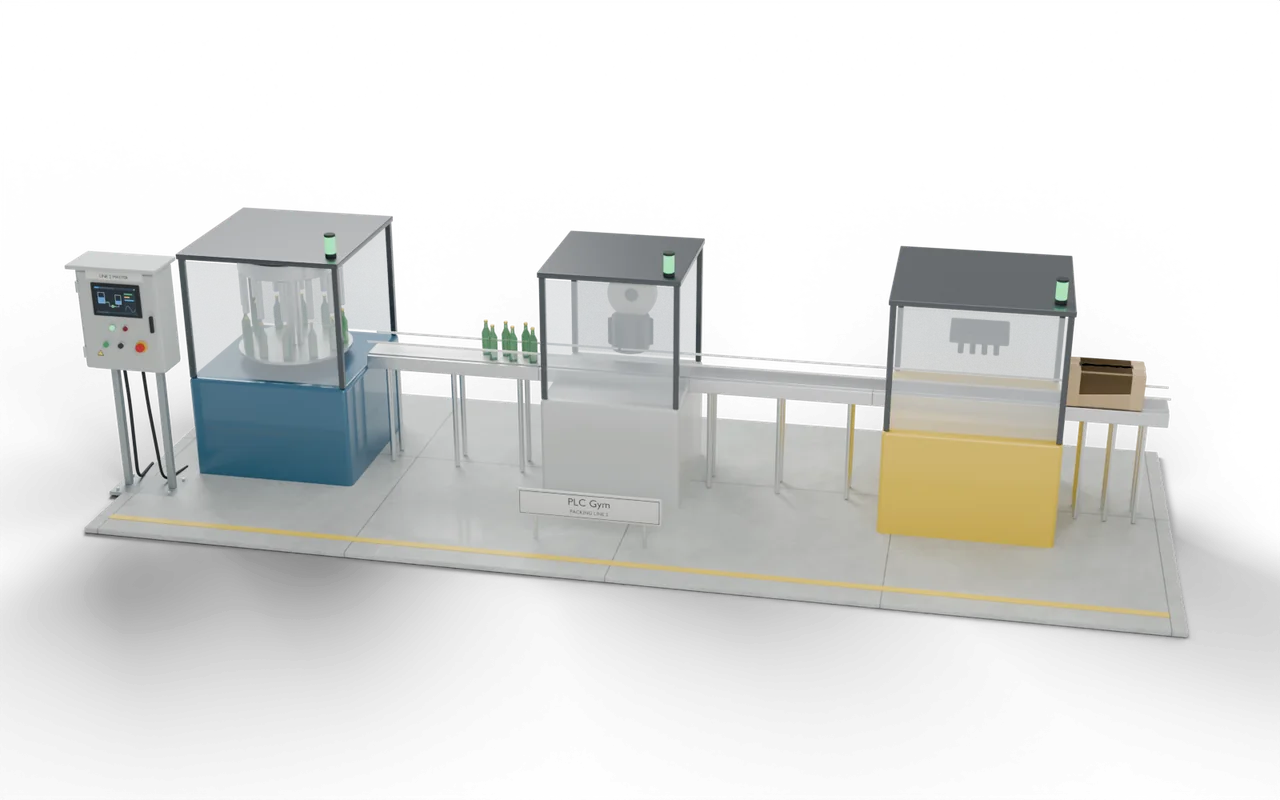
Coordinate three machines and two buffers as one line.
Start the line from the end, pace the labeller from Buffer 1, protect both buffers from overflowing, ride through jams without breaking bottles, and run the line out on Stop.
 Pro mission
Start from the end of the line
Test 1 of 5StartStart the lineOFFLabellerOKInputONPackerOKInputONFillerRunRun the fillerON- Level
- Expert
- Time
- About 90 min
- Reward
- +1200 XP
- Rig
- 3D packaging line control
- Siemens editors
- SCL, LAD
- Rockwell editors
- Structured Text, Ladder
- Course stage
- 30. Machine lab 5: expert systems
What the tests check
- Starts from the end of the line: packer, labeller after 2 s, filler after 4 s.
- Labeller speed follows Buffer 1, kept between 2 and 5 bottles/s.
- Filler slows at 30 and stops at 36, restarting below 28.
- Labeller holds at Buffer 2 ≥ 36 and needs LabellerOK.
- Stop runs both buffers empty before stopping everything.
- Try it Use the buttons below the model and watch the rig respond.
- Test solution Every check runs on your code in one press.
- Replay If one fails, step through it one scan at a time to see why.
Where you’d see this on site
Every packaging line has a line controller doing this. Tuning the buffer levels and speeds is how plants find extra output without buying machines.
A filler that stops loses product and time it can never get back. A buffer that overruns throws bottles on the floor. A line that stops all at once leaves half-labelled product in every machine.
On a packaging line the filler sets the pace: it is the most expensive machine, and stopping it wastes product. Every other machine runs a little faster and is paced by how full the buffers around it are, so the filler is never starved or blocked.
- Filler4 bottles/s
- Buffer 140 bottlesYou are here
- LabellerUp to 5/s
- PackerCases of 12
On a real site: places, parts and safety
- Bottling and canning lines
- Food and pharma packing halls
- Any line of machines joined by conveyors
Each machine has its own guards and safety circuit; the line controller only coordinates them.
Restarting a machine after a jam is the operator's decision: the line controller never restarts a machine whose guard is open.
The sizes, timings and cutaways are teaching choices, not a drawing of any one real installation.
Next in the course
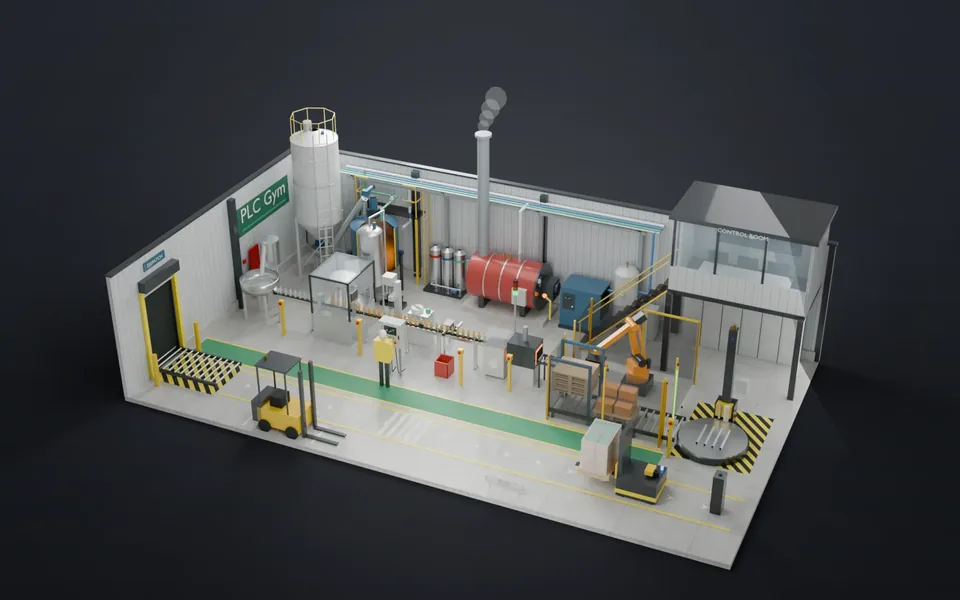 61Run the whole factoryStart-up, batching, bottling, rejects, robot, wrapper, AGV and safety: one programme for the whole plant.Expert · 240 min · +3000 XP
 56Three pumps, one wellStage pumps on an analogue level, share the hours and survive failures.Advanced · 70 min · +900 XP
 55Bay A to bay BPosition three crane axes from their encoders and move plates on a magnet.Advanced · 60 min · +750 XP
 54Clean, recover, rinseRun a CIP recipe with hold and resume, routing every litre by conductivity.Advanced · 60 min · +750 XP