The right bottle, every time
Track items by encoder through a queue, and verify every reject.
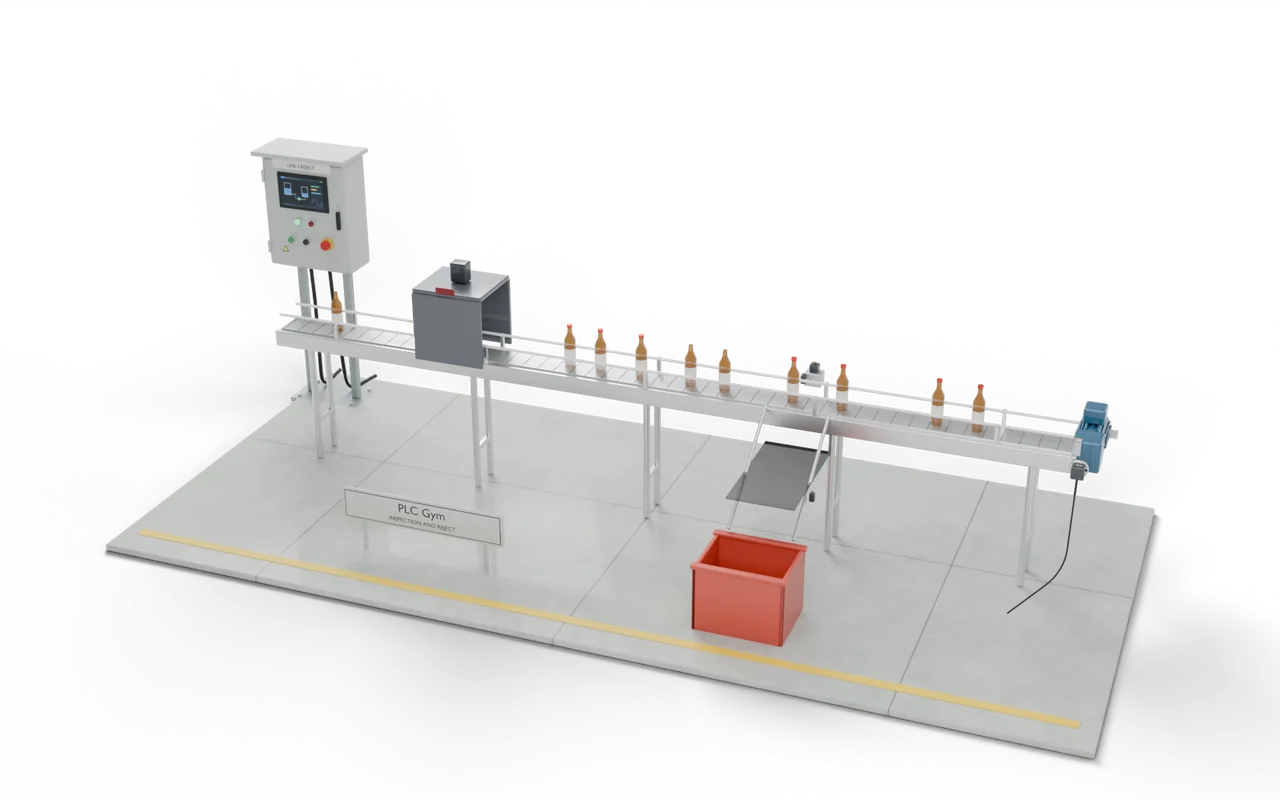
Reject every bottle the camera fails, and only those, with up to ten bottles between camera and jet, a belt that changes speed, bottles taken off by hand, and a confirm eye that must see every reject.
 Pro mission
Bad bottle out, good bottle on
Test 1 of 4StartStart the line (also clears a reject fault)OFFEncoderInput3700BottleAtVisionInputOFFRunRun the conveyorON- Level
- Expert
- Time
- About 90 min
- Reward
- +1200 XP
- Rig
- 3D encoder tracking reject system
- Siemens editors
- SCL, LAD
- Rockwell editors
- Structured Text, Ladder
- Course stage
- 30. Machine lab 5: expert systems
What the tests check
- Every bottle is queued with its encoder count at the trigger eye.
- The camera's late answer marks the right (newest) bottle.
- Bad bottles get 30 mm of air exactly 2135 mm later; good ones never do.
- A bottle that is no longer there is not blasted.
- An unconfirmed reject latches RejectFail and stops the line.
- Try it Use the buttons below the model and watch the rig respond.
- Test solution Every check runs on your code in one press.
- Replay If one fails, step through it one scan at a time to see why.
Where you’d see this on site
Every packing line with a checkweigher, metal detector or vision system has this tracking. It is one of the most common things a commissioning engineer gets called out to fix.
Track by time and the first slow-down rejects the wrong bottle. Forget the late camera answer and you mark the bottle behind. Skip the confirm and a blocked nozzle lets bad product ship.
Bottling, food and pharma lines inspect every item and reject the bad ones further down the line. Because many items sit between the two, the controller keeps a queue of positions measured by an encoder on the conveyor, not by time.
- VisionTrigger, then result
- QueueEncoder positionsYou are here
- Jet2135 mm later
- ConfirmIn the bin
On a real site: places, parts and safety
- Bottling and canning lines checking fill and caps
- Pharma packing lines checking labels and codes
- Food lines with metal detectors and checkweighers
In food and pharma, a failed reject is a product safety event: lines stop rather than let a bad item through.
Air jets are loud and can blow fragments: real ones sit behind guards.
The sizes, timings and cutaways are teaching choices, not a drawing of any one real installation.
Next in the course
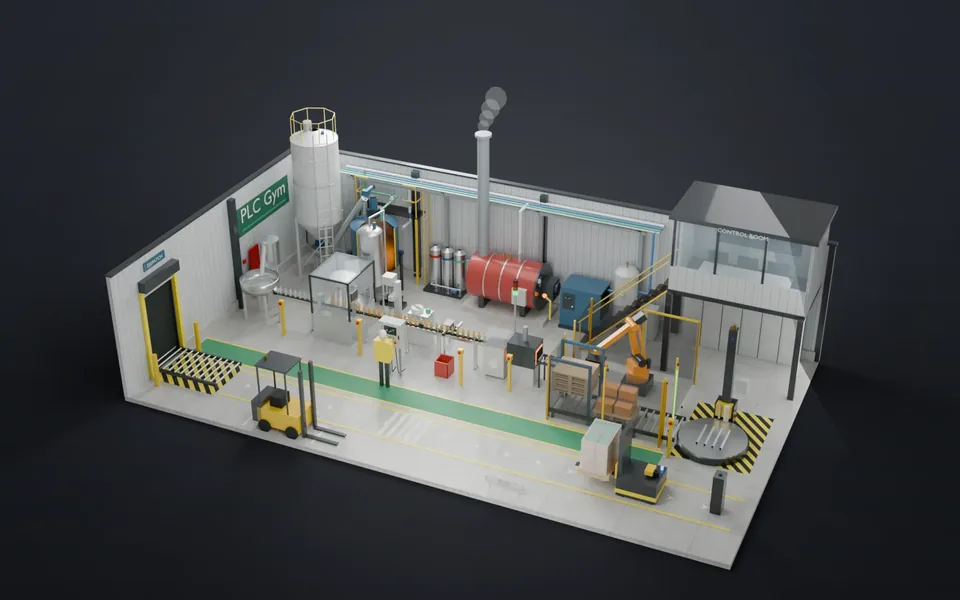 61Run the whole factoryStart-up, batching, bottling, rejects, robot, wrapper, AGV and safety: one programme for the whole plant.Expert · 240 min · +3000 XP
 56Three pumps, one wellStage pumps on an analogue level, share the hours and survive failures.Advanced · 70 min · +900 XP
 55Bay A to bay BPosition three crane axes from their encoders and move plates on a magnet.Advanced · 60 min · +750 XP
 54Clean, recover, rinseRun a CIP recipe with hold and resume, routing every litre by conductivity.Advanced · 60 min · +750 XP